 INNO fibre optic temperature sensors ,temperature monitoring systems.
- Fiber optic temperature monitoring systems use fluorescence-based sensing technology to deliver real-time, high-accuracy temperature data in high-voltage and electromagnetically harsh environments.
- Compared to thermocouples, RTDs, and infrared sensors, fiber optic temperature sensors offer complete EMI immunity, intrinsic electrical isolation, and a service life exceeding 25 years with zero maintenance.
- INNO (FJINNO) is a specialized manufacturer with 20+ years of industry experience, 3000+ installed systems worldwide, and exports to 15+ countries across Asia, Europe, the Americas, the Middle East, and Oceania.
- Applications span power transformers, switchgear, GIS equipment, generators, HVDC systems, semiconductor processing, MRI medical systems, battery energy storage, and aerospace environments.
- Product lines include fluorescent fiber optic temperature sensor probes, multi-channel monitoring hosts, dry-type transformer temperature controllers, distributed fiber optic systems, and fully customizable OEM/ODM solutions.
- All systems are manufactured under ISO 9001/14001/27001/45001, CE, EMC, and RoHS certifications, ensuring global compliance and reliability.
- Flexible partnership models are available, including distributor programs, OEM private-label manufacturing, ODM co-development, and localized system integration.
Table of Contents
- 1. What Is a Fiber Optic Temperature Monitoring System?
- 2. About INNO — A Trusted Fiber Optic Temperature Sensor Manufacturer
- 3. Why Choose Fiber Optic Temperature Monitoring?
- 4. Fiber Optic vs. Thermocouple vs. RTD vs. Infrared: Technical Comparison
- 5. Key Technical Specifications
- 6. Complete Product Portfolio
- 7. Power & Energy Industry Applications
- 8. Industrial & Equipment Manufacturing Applications
- 9. Medical & Life Sciences Applications
- 10. Renewable Energy & Battery Industry Applications
- 11. Extreme Environments & Advanced Applications
- 12. Infrastructure Monitoring Applications
- 13. Customization, OEM/ODM & Global Partnership
- 14. Real-World Project Cases & Engineering References
- 15. Why Choose INNO as Your Fiber Optic Temperature Monitoring Partner
- 16. Frequently Asked Questions (FAQ)
1. What Is a Fiber Optic Temperature Monitoring System?

A fiber optic temperature monitoring system is a complete temperature measurement solution built on fiber optic sensing technology. The system employs fluorescent fiber optic temperature sensor probes to detect temperature changes at critical measurement points, while optical fibers serve as the signal transmission medium, delivering data to a centralized temperature measurement host (demodulator) for signal processing, data acquisition, and real-time monitoring.
Unlike conventional electrical temperature sensors that rely on metallic conductors, fiber optic systems use light-based signal transmission. This fundamental difference gives fiber optic temperature measurement devices three defining advantages: complete electrical isolation, total immunity to electromagnetic interference (EMI), and inherently safe operation in high-voltage environments. These properties make fluorescent fiber optic temperature measurement the preferred choice for monitoring critical assets where traditional sensors simply cannot perform reliably.
How Does Fluorescent Fiber Optic Temperature Sensing Work?

The underlying principle of the system is fluorescence lifetime decay. A pulsed light signal is transmitted through an optical fiber to a fluorescent sensing element at the probe tip. The fluorescent material absorbs the excitation light and re-emits fluorescence, with the decay time of this fluorescence being directly dependent on temperature. The fiber optic temperature monitoring host precisely measures this decay time and converts it into an accurate temperature reading. Because the entire sensing mechanism is optical — with no electrical current at the measurement point — the system is intrinsically safe, spark-free, and immune to electromagnetic noise from surrounding high-voltage equipment.
Fiber optic temperature monitoring systems are now widely deployed across power transformers, switchgear, GIS equipment, cable joints, HVDC systems, generators, industrial furnaces, semiconductor processing equipment, medical MRI systems, and renewable energy installations. By integrating fiber optic sensors, monitoring modules, and system software, the solution enables accurate point-type temperature monitoring, real-time condition assessment, and long-term equipment protection in the most demanding operating environments.
2. About INNO — A Trusted Fiber Optic Temperature Sensor Manufacturer

Fuzhou Innovation Electronic Science & Technology Co., Ltd. (INNO / FJINNO) is a high-tech enterprise specializing in the research, development, manufacturing, and global supply of fiber optic temperature sensors and temperature monitoring systems. Established in 2011 and headquartered in Fuzhou City, Fujian Province, China, the company has built a solid reputation over 20+ years of dedicated focus on fiber optic temperature sensing technology.
Manufacturing Capabilities & Certifications
INNO operates a 3000+ square meter manufacturing facility with over 100 highly skilled employees, including a dedicated R&D engineering team. The company has established industry-academia-research partnerships with Fuzhou University and other institutions, resulting in the successful development of fluorescent fiber optic temperature sensors with fully independent intellectual property rights. All products are manufactured under strict quality management systems, holding ISO 9001/14001/27001/45001, CE, EMC, and RoHS certifications to meet evolving international compliance standards.
Global Presence & Track Record
With 3000+ installed systems worldwide, INNO’s products have been exported to over 15 countries and regions, including the Philippines, South Korea, Malaysia, Japan, Thailand, Singapore, Indonesia, Vietnam, the United Arab Emirates, South Africa, Australia, Brazil, Canada, the United States, Mexico, Germany, France, the Netherlands, Italy, and the United Kingdom. The company serves utilities, renewable energy facilities, transportation systems, and manufacturing plants across six continents, providing fiber optic temperature measurement systems trusted for accuracy, reliability, and long-term performance.
3. Why Choose Fiber Optic Temperature Monitoring?
A fiber optic temperature monitoring system delivers measurable value across three critical dimensions: equipment safety, operational reliability, and long-term cost control. By enabling accurate monitoring at critical thermal points inside high-voltage and industrial equipment, the system helps prevent unexpected failures, reduce unplanned downtime, and protect high-value assets.
Scalable Architecture & System Integration
Designed for demanding applications, the system supports scalable multi-channel configurations and seamless integration with existing monitoring platforms such as SCADA and PLC systems. Flexible sensor deployment and modular architecture allow straightforward adaptation to both new installations and retrofit projects, reducing implementation complexity and total project cost. Whether monitoring a single transformer or an entire substation, the fiber optic temperature measurement system can be configured to match the exact scope of each project.
Long-Term Cost Benefits
With stable long-term performance and minimal maintenance requirements, fiber optic temperature monitoring systems provide a cost-effective solution for condition-based maintenance and digital asset management. The 25+ year service life, zero maintenance and calibration needs, and early hot-spot detection capabilities help organizations achieve return on investment within 3–5 years through avoided failures and extended equipment life. Multi-channel capability further reduces per-point monitoring costs, making the technology economically viable even for large-scale deployments.
4. Fiber Optic vs. Thermocouple vs. RTD vs. Infrared: Technical Comparison
Selecting the right temperature sensing technology for critical equipment monitoring requires a clear understanding of each method’s strengths and limitations. Below is a detailed comparison of fiber optic temperature sensors, thermocouples, resistance temperature detectors (RTDs), and infrared sensors — evaluated across the parameters that matter most in high-voltage and industrial environments.
Fiber Optic Temperature Monitoring — Advantages
Fiber optic temperature monitoring systems deliver complete EMI immunity, enabling stable and accurate measurement even in the strongest electromagnetic environments found around transformers, switchgear, and power electronics. The sensing mechanism is fully non-conductive and spark-free, providing intrinsic electrical isolation that eliminates ground loop risks and electrical hazards. The sensors withstand extreme high-voltage conditions exceeding 100 kV, and the corrosion-resistant optical probes perform reliably in harsh, chemically aggressive, and high-humidity environments. The compact temperature monitoring host design allows easy integration into existing control cabinets. With a service life exceeding 25 years and no requirement for periodic recalibration, fluorescent fiber optic sensors provide genuinely maintenance-free operation with stable accuracy throughout their entire operational lifetime.
Thermocouple — Limitations
Thermocouples use metallic junctions that are inherently susceptible to electromagnetic interference, producing signal noise and measurement errors in high-EMI environments. The conductive metal elements introduce ground loop risks and potential electrical hazards when installed in high-voltage areas. Thermocouples cannot operate safely in extremely high-voltage environments due to electrical conduction through the sensor leads. Response time is slower due to the larger thermal mass of the junction and protective sheath. Complex wiring configurations — typically 3-wire or 4-wire setups with lead resistance compensation — increase installation costs and maintenance requirements.
RTD — Limitations
RTDs suffer from self-heating effects caused by the measurement current passing through the sensing element, which reduces accuracy particularly in low-flow or oil-immersed conditions. Like thermocouples, RTDs require complex multi-wire configurations with careful lead resistance compensation, increasing installation complexity. The larger thermal mass and protective sheath result in slower temperature response compared to fiber optic temperature probes. Long cable runs introduce significant resistance errors requiring additional compensation circuits and calibration. Each RTD requires separate wiring and signal conditioning, making large-scale multi-point monitoring prohibitively expensive. Platinum element resistance also drifts over time due to thermal cycling and mechanical stress, requiring periodic recalibration throughout the sensor’s life.
Infrared Temperature Sensor — Limitations
Infrared sensors measure only surface temperatures and cannot detect internal hot spots within transformer windings, insulation systems, or oil-filled equipment. They require a clear optical path (line-of-sight) to the target, which is blocked by oil, insulation materials, tank walls, and enclosed structures. Measurement accuracy is heavily dependent on surface emissivity, which changes unpredictably with oil films, oxidation, contamination, and aging. Environmental factors including ambient temperature, humidity, dust, and oil mist degrade measurement reliability. Infrared sensors cannot be embedded inside equipment or submerged in oil for direct contact temperature measurement, and their accuracy decreases significantly with distance and viewing angle, requiring precise mounting and frequent calibration adjustments.
5. Key Technical Specifications
The following specifications represent the standard configuration of INNO’s fiber optic temperature measurement system. All key parameters are customizable to meet specific application requirements.
System Specifications Overview
The standard measurement accuracy is ±1°C, with customization available for applications requiring higher precision. The operating temperature range spans –40°C to +260°C, also customizable for specialized high-temperature or cryogenic applications. Fiber optic cable lengths support 0 to 80 meters from sensor to host, with custom extensions available. Response time is under 1 second, enabling real-time thermal event detection. The fluorescent fiber optic temperature sensor probe features a compact diameter of 2–3 mm, suitable for installation in confined spaces including transformer windings and switchgear contact points. The system provides full electrical insulation with voltage withstand capability exceeding 100 kV.
System Configuration & Communication
Each fiber optic temperature measurement demodulator supports 1 to 64 monitoring channels, enabling scalable multi-point temperature acquisition from a single host unit. The standard communication interface is RS485 with Modbus RTU protocol, ensuring compatibility with SCADA, PLC, DCS, and other industrial monitoring platforms. Power supply options include AC 220V or DC 24V. The operating environment specification covers –20°C to +70°C ambient temperature with humidity tolerance up to 95% RH. Sensor probes carry an IP65 protection rating. The complete system — including the demodulator, fluorescent fiber optic sensors, display module, and monitoring software — holds CE, EMC, and ISO 9001 certifications. Designed service life exceeds 25 years under normal operating conditions.
6. Complete Product Portfolio
INNO offers a comprehensive product range covering every component of a fiber optic temperature monitoring system — from individual sensor probes to complete turnkey monitoring solutions, distributed fiber optic systems, and custom-developed software platforms.
Fiber Optic Temperature Sensors
The sensor product line includes fluorescent fiber optic temperature sensor probes in standard and custom configurations, armored fiber optic temperature sensors specifically designed for oil-immersed transformer winding installations, fiber optic temperature sensors for busbar and bolt connections in switchgear and panel applications, and single-channel fluorescent fiber optic temperature sensing modules for OEM integration into third-party equipment and control systems.
Fiber Optic Temperature Monitoring Systems
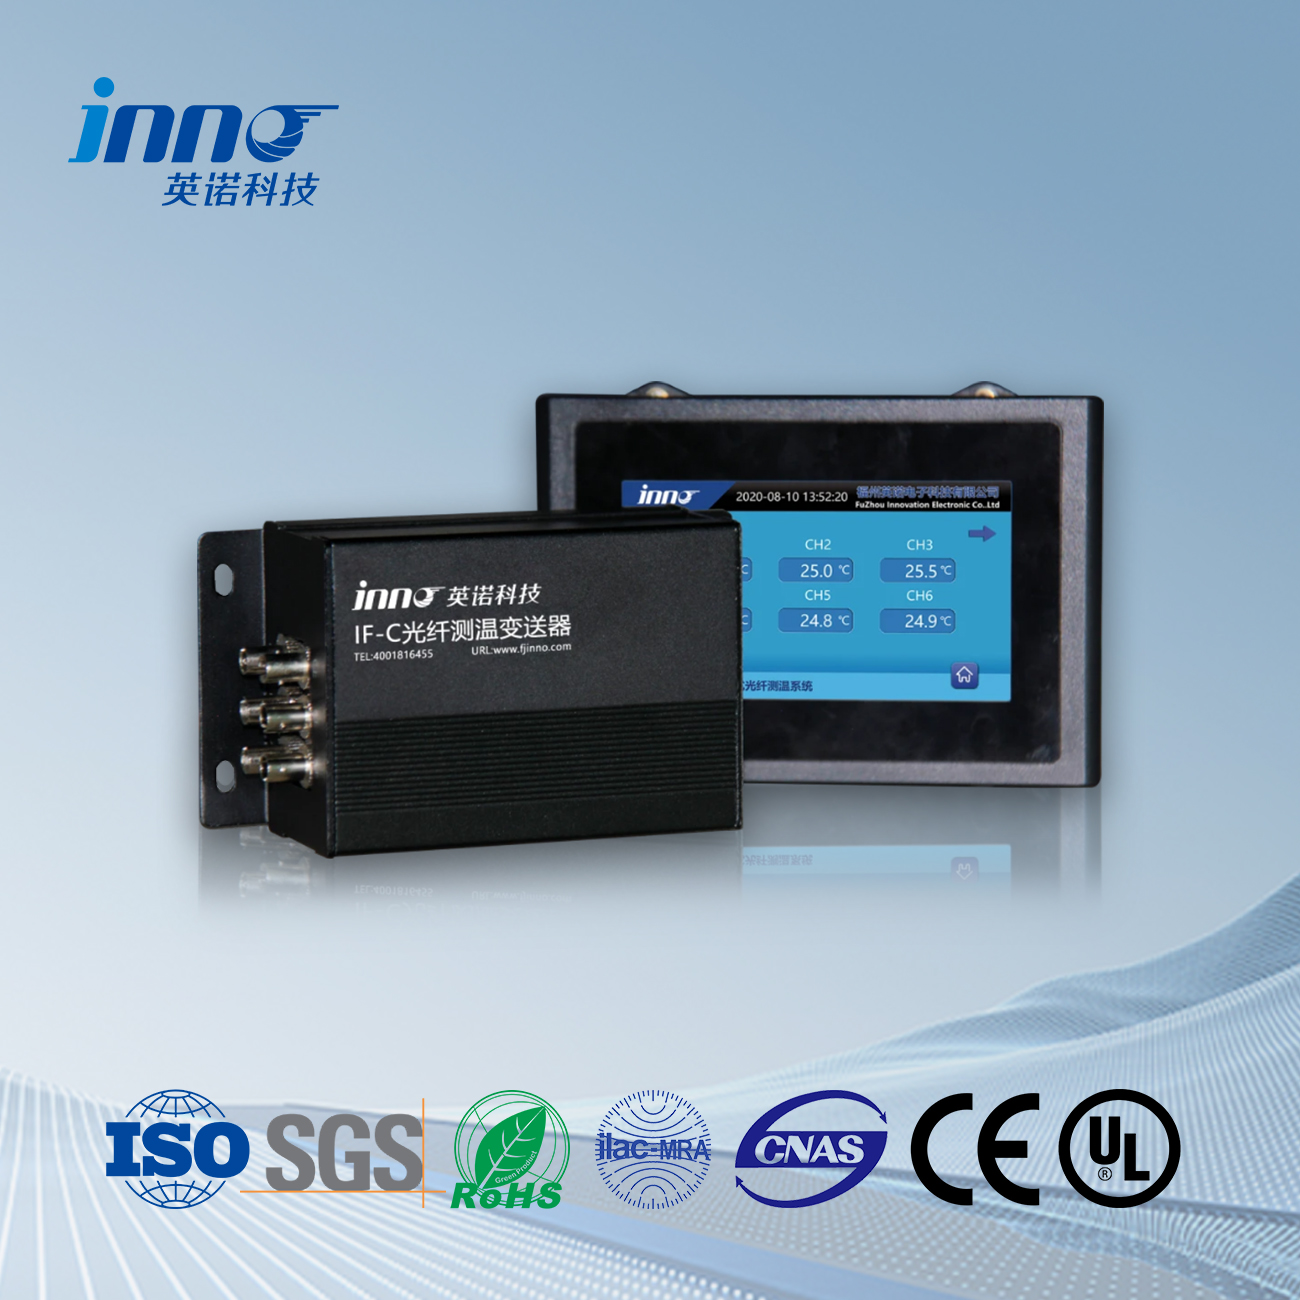
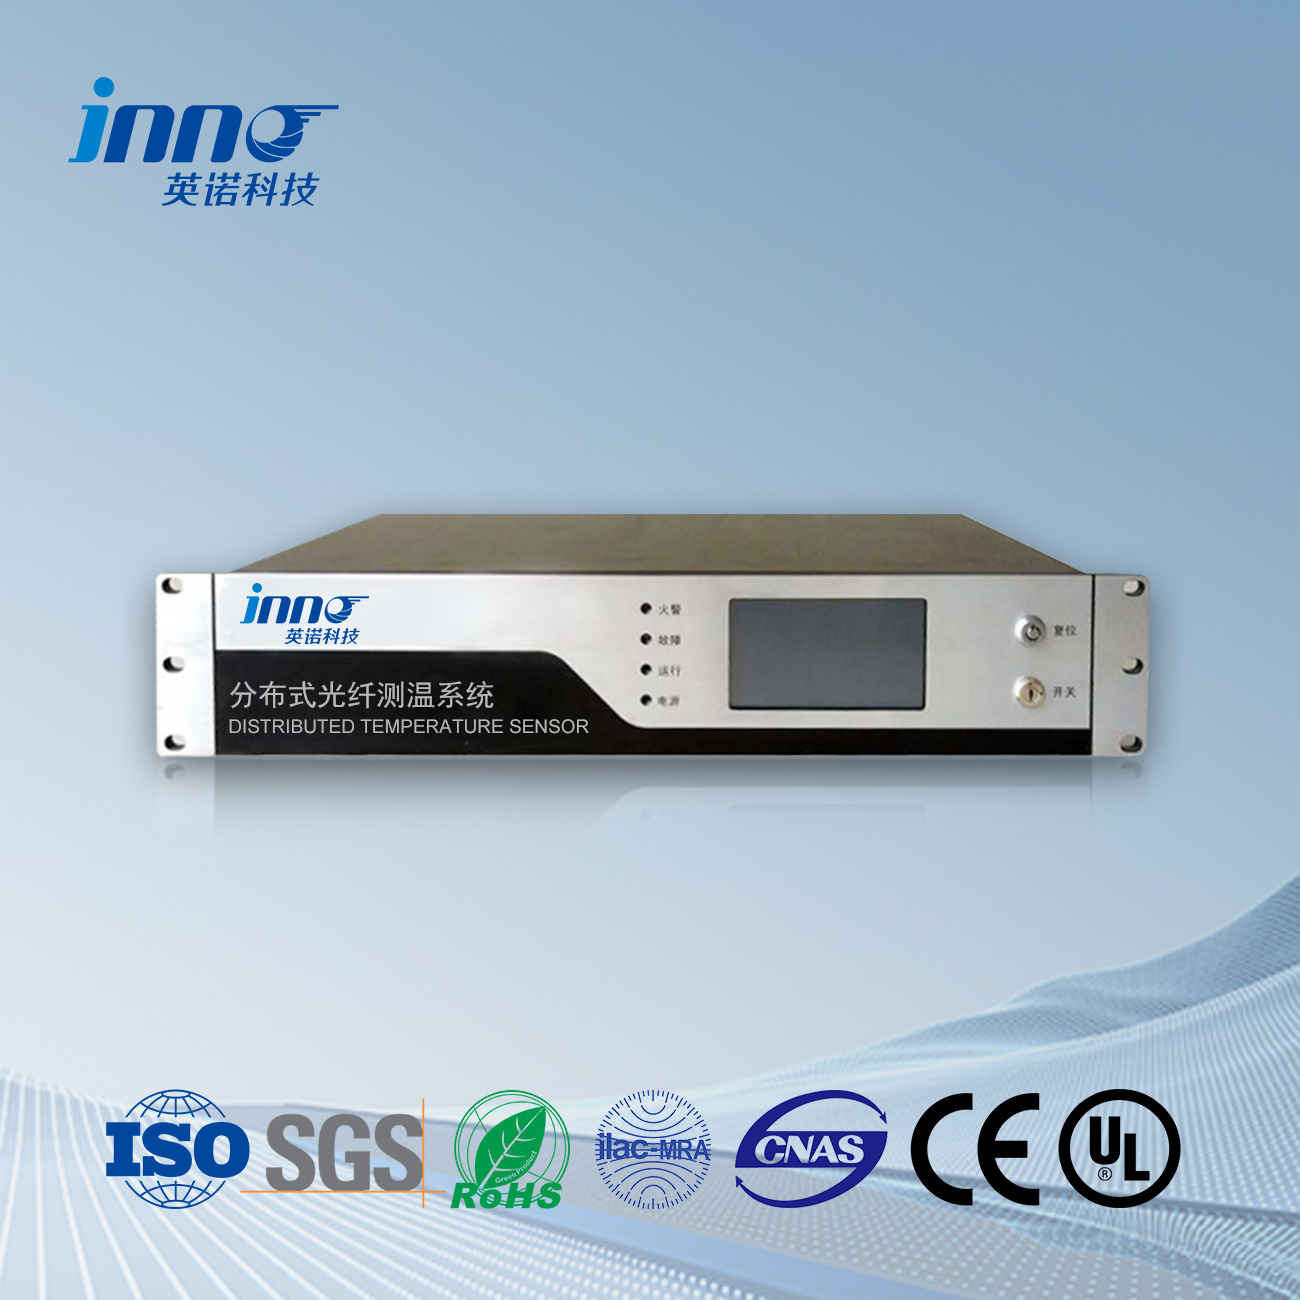
The system-level product range includes a 6-channel fiber optic temperature monitoring device for multi-point measurement applications, a fiber optic temperature measurement display-integrated host combining signal processing and visual readout in a single compact unit, a microwave electromagnetic anti-interference fiber optic temperature measurement system engineered for extreme EMI environments, and a fiber optic temperature measurement system for dry-type transformer windings with integrated intelligent monitoring capabilities. INNO also offers customized fiber optic temperature measurement module development for clients requiring tailored sensing solutions.
Specialized Application Systems
Purpose-built systems address specific industry needs: the intelligent monitoring device for polycrystalline silicon dry-type transformers, the dry-type reactor fiber optic temperature measurement device, the fiber optic temperature measurement system for transformers in box-type substations, the fiber optic temperature measurement system for switchgear, and fiber optic temperature measurement solutions for semiconductor processing equipment heating. Each system is pre-configured for its target application while remaining customizable for project-specific requirements.
Transformer Temperature Controllers
Complementing the fiber optic product line, INNO manufactures dedicated dry-type transformer temperature controllers including the BWDK-326 and BWDK-S201 series, along with oil-immersed transformer fiber optic temperature monitoring systems. These controllers provide automated fan control, over-temperature alarming, and trip protection functions essential for transformer thermal management.
Distributed Fiber Optic Systems
For large-scale linear infrastructure monitoring, INNO provides the BOTDR/A distributed fiber optic temperature and strain sensing system, the distributed fiber optic pipeline leakage temperature monitoring system, the distributed fiber optic perimeter security monitoring system, and the distributed fiber optic vibration monitoring system. These systems enable continuous temperature and vibration sensing over distances of several kilometers using a single optical fiber cable.
Software & Cloud Platform
INNO provides customized cloud platform development for fiber optic temperature measurement system software, enabling remote data acquisition, real-time visualization, multi-level alarm management, historical trend analysis, and integration with enterprise asset management platforms. The software supports RS485/Modbus RTU data upload and can be tailored to client-specific interface requirements, branding, and functional specifications.
7. Power & Energy Industry Applications
Power and energy systems operate under high voltage, strong electromagnetic interference, and continuous load conditions that demand exceptional measurement reliability. Fluorescent fiber optic temperature sensing technology provides the electrically isolated, EMI-immune condition monitoring that critical power assets require. Integrated with measurement hosts and monitoring systems, fiber-based solutions support fault prevention, asset health assessment, and reliable operation across transmission, distribution, and power conversion infrastructures.
Power Transformers
In transformer applications — including dry-type transformers, oil-immersed transformers, and distribution transformers — fiber optic temperature sensors and point-type probes are installed near windings, cores, and insulation hot spots. Temperature data is transmitted through optical fibers to a centralized measurement host, forming a complete fiber optic temperature monitoring system that supports insulation aging analysis, overload evaluation, and long-term asset management. Direct winding hot-spot temperature measurement — rather than reliance on top-oil temperature modeling — provides the most accurate thermal picture of transformer health.
Switchgear & Circuit Breakers
Switchgear and circuit breakers — including vacuum circuit breakers and SF₆ circuit breakers — involve frequent switching operations and extremely strong electromagnetic environments. Fluorescent fiber optic temperature probes applied to contacts, arc chambers, busbar connections, and operating mechanisms enable stable point monitoring without electrical interference, helping identify abnormal conditions related to contact degradation, connection loosening, or mechanical wear before they escalate into failures.
GIS Equipment
Gas-insulated switchgear (GIS) features fully sealed structures and extremely high internal electric field intensities. Fluorescent fiber optic sensors provide reliable internal temperature monitoring without introducing any conductive components into the sealed gas compartment. Combined with dedicated interrogation units, these sensors support long-term condition assessment of critical GIS modules, bus sections, and circuit breaker compartments.
Cable Joints & Terminations
Cable joints and terminations are particularly sensitive to installation quality and load variation, with localized overheating representing a leading cause of cable failure. Fiber optic sensing solutions enable continuous temperature monitoring at these critical junctions, with optical fibers transmitting data over long distances to centralized monitoring systems, supporting early fault detection and overall network reliability improvement.
Power Reactors & Shunt Reactors
Reactors — including series reactors and smoothing reactors — operate under high inductive loads and intense electromagnetic stress. Fiber optic temperature sensors installed near windings and structural components provide reliable localized temperature monitoring, supporting cooling performance evaluation, thermal margin assessment, and operational stability analysis.
Generators
In generator applications — covering synchronous generators and turbo generators — fiber optic probes can be embedded at critical stator and rotor winding locations. Integrated into a fiber optic temperature monitoring system, these probes provide accurate internal temperature data to support performance optimization, insulation protection, and long-term equipment reliability. The small probe diameter (2–3 mm) enables installation in tight stator slot spaces without affecting the machine’s electromagnetic performance.
HVDC Equipment
HVDC converter valves and valve hall equipment operate under extremely high electric fields and fast-switching conditions where conventional sensors are unreliable. Fiber optic temperature monitoring modules integrated into valve assemblies and auxiliary equipment provide stable, interference-free measurement performance, supporting condition assessment and reliability improvement of HVDC transmission systems.
Capacitor Banks
Capacitor-based reactive power compensation systems operate in harmonic-rich environments where localized heating can develop undetected. Fiber optic temperature sensors and probes enable accurate point monitoring inside capacitor units, with data collected by the measurement host to support stable operation and optimized maintenance scheduling.
8. Industrial & Equipment Manufacturing Applications
Industrial equipment operates under demanding conditions including strong electromagnetic interference, extreme temperatures, and vacuum environments, imposing strict requirements on measurement accuracy and sensor reliability. Fiber optic sensing technology, with its inherent electrical isolation, EMI immunity, and harsh-environment resilience, provides stable point-type temperature monitoring for critical industrial components. Integrated with measurement hosts and monitoring systems, fiber-based solutions support thermal management optimization, fault early warning, and full-lifecycle equipment health management.
Motor Winding Temperature Monitoring
Motor windings — particularly in high-voltage and large motors — operate under high current density and strong electromagnetic fields, making them susceptible to insulation thermal aging, a leading cause of motor failure. Fiber optic temperature sensors can be embedded directly into stator slots and critical winding end positions to enable real-time hot-spot monitoring. Measurement data transmitted via optical fiber to a dedicated interrogation unit forms a complete monitoring system that supports overheat alarming, insulation life assessment, and preventive maintenance management.
VFD & Power Module Temperature Monitoring
Variable frequency drives (VFDs) and high-power modules generate significant heat during high-frequency switching operations, and localized overheating can cause component failure or system shutdown. Fluorescent fiber optic temperature probes installed on heat sink substrates, busbars, and critical contact points provide accurate point temperature measurement completely free from electromagnetic interference. Integrated with the monitoring system, real-time thermal management analysis supports cooling performance optimization and equipment reliability improvement.
IGBT & SiC Power Device Junction Temperature Monitoring
IGBT modules and SiC MOSFET devices operate under high voltage, high frequency, and high current conditions, where junction temperature directly affects device lifespan and system safety. Fiber optic temperature probes can be positioned close to chip package surfaces or embedded within modules to achieve high-accuracy real-time monitoring of junction and case temperatures. Data transmitted to the fiber optic temperature monitoring system supports thermal resistance analysis, power cycle lifetime prediction, and over-temperature protection control.
Industrial Furnace Temperature Monitoring
Industrial furnaces — including heat treatment, annealing, sintering, and smelting furnaces — require uniform thermal field distribution to ensure product quality and process consistency. High-temperature-resistant fiber optic temperature sensors deployed at critical zones within the furnace chamber, near heating elements, and at workpiece positions enable synchronized multi-point temperature acquisition. Real-time thermal field distribution analysis via the fiber optic measurement host supports process parameter optimization, energy consumption control, and furnace health assessment.
Semiconductor Equipment Temperature Monitoring
Semiconductor manufacturing equipment — including lithography, etching, CVD, and PVD process chambers — demands extremely high temperature uniformity and control precision, as minor temperature deviations directly impact process yield and product performance. Fiber optic temperature probes, with their inherent electrical isolation and EMI immunity, can be installed at process chamber walls, electrostatic chucks, and gas shower heads to achieve precise monitoring in nanoscale process environments. Integrated with the temperature monitoring system, they support thermal uniformity analysis and closed-loop temperature control optimization.
Vacuum Environment Temperature Monitoring
In vacuum chambers, vacuum furnaces, and electron beam or ion beam equipment, conventional electrical sensors face challenges including outgassing contamination, discharge risks, and signal feedthrough difficulties. Fiber optic temperature sensors require no electrical power supply at the sensing point and involve no metallic conductor feedthroughs, enabling hermetically sealed installation via vacuum feedthrough fittings that are fully compatible with ultra-high vacuum conditions. Fluorescent fiber optic probes provide stable contact temperature measurement of critical internal components under full vacuum insulation conditions.
Industrial Robot & Automation Equipment
Industrial robots and automation systems operating continuously at high speed and high load are prone to thermal accumulation in core components such as joint motors, servo drives, and reducers. Compact fiber optic temperature probes can be integrated into confined mechanical joint spaces and operate stably in strong electromagnetic environments. Real-time thermal state monitoring of each axis via the fiber optic temperature monitoring system supports thermal compensation strategy development, preventive maintenance scheduling, and overall system reliability improvement.
High-Power Laser Equipment
High-power laser systems — including solid-state lasers and fiber lasers — generate significant thermal effects in gain media, pump modules, and resonator structures under high-power pumping conditions. Fiber optic temperature probes with excellent radiation resistance can be installed at laser crystals, fiber coiling regions, and critical positions on cooling substrates. Combined with the measurement host, they support optimized thermal management system design, output power stability control, and long-term laser operation management.
9. Medical & Life Sciences Applications

Medical environments present unique challenges including strong magnetic fields, high-frequency RF signals, and strict biosafety requirements. Fiber optic temperature sensing technology, with its inherent EMI immunity, complete electrical isolation, and ultra-slim probe design, has established itself as the core temperature monitoring solution for high-precision medical applications such as MRI, ablation therapies, and interventional procedures.
MRI Temperature Monitoring
Fiber optic temperature sensors are completely immune to the strong magnetic fields and RF signals present in MRI environments. They enable safe and accurate real-time temperature monitoring during MRI scanning without disrupting the imaging process. For MRI-guided thermal therapies, fiber optic sensing represents the only reliable method for continuous temperature feedback, ensuring treatment safety and efficacy while maintaining full imaging capability.
HIFU & Ablation Real-Time Temperature Monitoring
Fiber optic temperature monitoring systems provide millisecond-level real-time temperature feedback during high-intensity focused ultrasound (HIFU) and various ablation therapies. This rapid response enables precise thermal dose control at the target treatment zone, effectively protecting surrounding healthy tissue and enhancing treatment outcomes. The complete absence of electromagnetic interference ensures that temperature readings remain accurate throughout the entire procedure.
Radiofrequency Ablation (RFA) Temperature Monitoring
Radiofrequency ablation generates intense electromagnetic fields that render conventional electronic temperature sensors unreliable. Fiber optic temperature probes, with their inherent EMI immunity, can be placed directly within the ablation zone to provide stable and accurate temperature monitoring throughout the procedure. This capability is essential for ensuring precise ablation coverage while protecting adjacent healthy tissue from thermal damage.
Medical Catheter & Implantable Temperature Monitoring
Ultra-slim fiber optic probes (2–3 mm diameter) can be integrated into medical catheters or miniature implantable devices to meet the demands of minimally invasive in-vivo monitoring. With excellent biocompatibility, these probes are suitable for a wide range of interventional procedures — including cardiac, oncological, and neurological applications — enabling long-term stable in-vivo temperature monitoring without introducing any electrical conductors into the patient’s body.
10. Renewable Energy & Battery Industry Applications
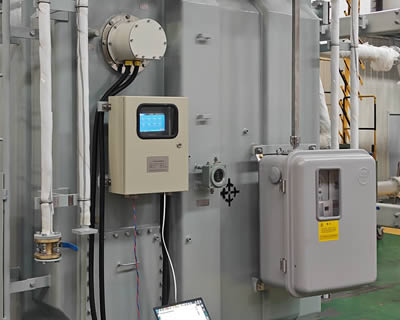
Renewable energy equipment and battery systems operate under high voltage, strong electromagnetic interference, and complex thermal management conditions. Fiber optic temperature sensing technology, with its EMI immunity, electrical isolation, fast response, and ultra-slim probe design, can be deployed deep inside battery cells, energy storage cabinets, and critical components of power generation equipment to provide precise and continuous temperature data.
Wind & Solar Power Equipment
Wind turbines and photovoltaic inverters operate continuously in environments with strong electromagnetic interference and elevated voltage levels. Fiber optic temperature sensors installed at critical hot spots — such as generator windings, bearings, and inverter power modules — monitor temperature rise trends in real time, provide early warnings of overheating risks, and help extend equipment service life while reducing unplanned downtime and maintenance costs.
Power Battery Pack & Module Internal Monitoring
Fiber optic probes can be embedded directly inside battery cells and modules without affecting the battery structure or electrochemical performance, enabling multi-point, high-precision internal temperature monitoring. Accurate internal temperature data helps optimize BMS thermal management strategies, balance cell temperature distribution, extend battery cycle life, and ensure the safe and stable operation of electric vehicle battery systems and stationary energy storage installations.
Energy Storage Cabinet Thermal Runaway Monitoring
Thermal runaway in energy storage systems remains one of the primary causes of fire and explosion hazards in battery installations. Fiber optic distributed or multi-point temperature monitoring systems provide comprehensive, continuous monitoring of each battery module within storage cabinets. With millisecond-level response to abnormal temperature rises, these systems trigger alarms and activate protection mechanisms at the earliest stage of a thermal event, significantly reducing the risk of cascading thermal runaway propagation.
Fuel Cell Stack & Battery Safety Testing
The internal temperature distribution of fuel cell stacks directly affects reaction efficiency and service life. Fiber optic probes accurately collect in-stack temperature data without introducing electromagnetic interference to the electrochemical process. In battery safety abuse testing — including nail penetration, overcharging, and short-circuit tests — fiber optic temperature monitoring systems capture real-time temperature dynamics under extreme conditions, providing critical data for battery safety design validation and standards certification.
11. Extreme Environments & Advanced Applications
From aerospace and defense to oil and gas, chemical processing, and scientific research, fiber optic temperature sensing technology is solving measurement challenges that conventional sensors cannot address. The intrinsic safety, full electrical isolation, EMI immunity, and radiation resistance of optical fiber sensors make them the trusted choice for the most demanding, high-stakes operating environments.
Aerospace & Defense
Aerospace engines, spacecraft onboard equipment, radar high-power components, and missile-borne electronics demand sensors with extreme heat resistance, strong EMI immunity, and radiation tolerance. Fiber optic temperature sensors are compact, lightweight, and fully passive — operating stably under high-EMI, high-radiation, and thermally extreme conditions. They accurately monitor temperature rise trends at mission-critical components, providing essential data for aerospace system safety verification and defense equipment reliability assessment.
Scientific Research & Nuclear Facilities
In high-voltage experimental platforms, strong magnetic field facilities, particle accelerators, and nuclear power plants, conventional sensors are frequently compromised by electromagnetic interference, radiation damage, and extreme electric fields. Fiber optic temperature sensors — being non-conductive, EMI-immune, and radiation-resistant — operate reliably in these harsh research environments, delivering accurate real-time temperature data at critical measurement points to ensure research safety, data integrity, and nuclear facility operational integrity.
Oil, Gas & Chemical Industry
Oil and gas facilities involve flammable and explosive atmospheres, high-pressure pipelines, and confined or deep-well environments that demand intrinsically safe sensing solutions. Fiber optic systems require no electrical power at the sensing point and generate no sparks, making them inherently explosion-proof. They provide continuous real-time monitoring of reactor hot spots, critical pipeline nodes, and deep-well temperature profiles — helping prevent thermal runaway events and ensuring safe, stable production operations in hazardous environments.
12. Infrastructure Monitoring Applications
Beyond point-type temperature measurement, INNO’s distributed fiber optic sensing systems extend monitoring capabilities to large-scale linear infrastructure, enabling continuous temperature and vibration detection over distances of several kilometers using a single optical fiber cable.
Pipeline Leakage & Thermal Monitoring
The distributed fiber optic pipeline leakage temperature monitoring system detects abnormal temperature changes along heat and water pipelines, oil and gas transmission lines, and underground utility corridors. By identifying localized temperature anomalies that indicate leaks, the system enables rapid response and targeted maintenance, minimizing environmental damage and operational disruption.
Tunnel Cable Fire Detection
Distributed fiber optic temperature sensing (DTS) provides continuous linear temperature monitoring along tunnel cable trays and underground cable routes. The system detects localized hot spots and rapid temperature rises indicative of cable overloading, insulation degradation, or incipient fire conditions, triggering alarms well before temperatures reach dangerous levels.
Perimeter Security & Intrusion Monitoring
The distributed fiber optic perimeter security monitoring system and distributed fiber optic vibration monitoring system detect physical intrusion attempts, ground disturbances, and unauthorized access along perimeter fences, restricted areas, and critical infrastructure boundaries. The systems operate passively with no electrical components in the field, making them immune to electromagnetic jamming and suitable for security-critical installations.
13. Customization, OEM/ODM & Global Partnership

INNO offers flexible cooperation models designed to serve the diverse needs of global partners, from independent distributors to large-scale system integrators and original equipment manufacturers.
OEM & Private-Label Manufacturing
As a professional OEM/ODM fiber optic sensor manufacturer, INNO provides complete private-label manufacturing services. Clients can specify custom branding, packaging, documentation, and product configurations while benefiting from INNO’s established manufacturing processes, quality systems, and testing capabilities. From fiber optic temperature sensor probes to complete monitoring system assemblies, every product can be manufactured to client specifications.
ODM Co-Development
For partners requiring customized sensing solutions, INNO’s engineering team collaborates on ODM product development — from modified sensor probe designs and specialized fiber optic cable assemblies to custom temperature measurement module development, tailored monitoring host configurations, and application-specific cloud platform software development. The company’s in-house R&D capabilities and university research partnerships enable rapid development cycles and technical innovation.
Distributor & System Integrator Programs
INNO supports distributor and agent partnerships with competitive pricing structures, marketing support, technical training, and dedicated account management. System integrators receive comprehensive technical documentation, integration support, and flexible product configurations to incorporate fiber optic temperature monitoring capabilities into their own solution offerings. The company provides one-on-one support through a skilled sales team with rapid quote response times.
Custom Development Capabilities
Specific customization services include fiber optic temperature measurement module development for integration into third-party equipment, RS485 interface development and customization for specialized communication protocols, cloud platform software customized development for remote monitoring and data analytics, and custom sensor probe configurations for unique installation geometries and environmental conditions.
14. Real-World Project Cases & Engineering References
INNO’s fiber optic temperature monitoring systems are validated through extensive real-world deployments across multiple industries and geographies. The following project cases demonstrate the practical application and proven performance of the technology in demanding operational environments.
Transformer Fiber Optic Temperature Controller Installation
Multiple installations of fiber optic temperature controllers on power transformers, providing continuous winding hot-spot temperature monitoring. These deployments demonstrate the system’s ability to deliver accurate thermal data for transformer load management, insulation life assessment, and automated cooling control in live substation environments.
Busway Distributed Fiber Optic Temperature Monitoring
A distributed fiber optic temperature monitoring system for busway was deployed in a real-world project, providing continuous linear temperature sensing along the entire busway length. The system identifies localized hot spots at connection joints and load concentration points, supporting maintenance prioritization and preventing unexpected busway failures.
Generator Stator Winding Monitoring
A fluorescent fiber optic temperature monitoring system was installed for rotating machine applications, specifically monitoring generator stator winding temperatures. The ultra-slim probes were embedded within stator slots to provide direct winding temperature measurement, enabling real-time thermal protection and performance optimization of the generating unit.
Dry-Type Transformer Installation Case
A complete fiber optic temperature monitoring system for dry-type transformers was deployed with multi-point sensing on transformer windings. The installation case demonstrates straightforward sensor mounting procedures and reliable integration with existing transformer protection and control systems, confirming that standard electrical technicians can complete the installation with minimal training.
15. Why Choose INNO as Your Fiber Optic Temperature Monitoring Partner
Selecting a fiber optic temperature monitoring system supplier is a long-term decision that affects equipment safety, monitoring reliability, and total cost of ownership for decades. INNO (FJINNO) has built its reputation as a trusted manufacturing partner through consistent product quality, technical depth, and responsive global service.
Independent R&D and Intellectual Property
INNO’s in-house R&D team, reinforced by industry-academia-research partnerships with Fuzhou University and other institutions, has developed fluorescent fiber optic temperature sensors with fully independent intellectual property rights. This R&D foundation ensures continuous product improvement, rapid customization capability, and deep technical expertise that benefits every client engagement.
Proven Manufacturing Quality
All products are manufactured under rigorous quality management systems certified to ISO 9001/14001/27001/45001, CE, EMC, and RoHS standards. With 3000+ systems installed and operating worldwide, INNO’s manufacturing processes are proven at scale across diverse application environments and climate conditions.
Comprehensive Product Range
From individual fluorescent fiber optic sensor probes and single-channel sensing modules to multi-channel temperature monitoring systems, distributed fiber optic sensing platforms, transformer temperature controllers, and custom cloud monitoring software, INNO provides a one-stop solution that eliminates multi-vendor complexity and ensures full system compatibility.
Global Delivery & Technical Support
With products exported to 15+ countries and 3000+ installed systems, INNO provides professional packaging, complete documentation, remote commissioning assistance, and 24/7 technical support for successful deployment worldwide. Experienced engineers and flexible production methods enable shorter lead times and faster delivery compared to larger, less responsive competitors.
Contact INNO
To discuss your fiber optic temperature monitoring requirements or request a customized solution quotation, contact the INNO team directly:
Email: web@fjinno.net
WhatsApp / WeChat: +8613599070393
Phone: +8613599070393
Company Phone: +8659183846499
Address: No. 12 Xingye West Road, Fuzhou City, Fujian, China
Website: www.fjinno.net
16. Frequently Asked Questions (FAQ)
Q1: What is a fiber optic temperature monitoring system and how does it work?
A fiber optic temperature monitoring system uses fluorescence lifetime decay technology to measure temperature. A pulsed light signal travels through an optical fiber to a fluorescent sensing probe at the measurement point. The fluorescent material’s decay time changes with temperature, and the system’s demodulator converts this optical signal into precise temperature readings. Because the entire sensing chain is optical with no electrical current at the measurement point, the system provides complete electrical isolation and total immunity to electromagnetic interference.
Q2: How does fiber optic temperature measurement differ from infrared temperature sensing?
Fiber optic sensors measure internal temperatures directly at critical points inside equipment — including transformer windings, switchgear contacts, and motor slots — while infrared sensors can only measure surface temperatures and cannot penetrate tank walls, insulation, or oil to detect internal hot spots. Fiber optic systems are unaffected by line-of-sight obstructions, oil mist, dust, or emissivity variations, providing significantly more stable and reliable data for critical asset monitoring.
Q3: What are the main advantages of fiber optic temperature sensors over thermocouples and RTDs?
Fiber optic temperature sensors offer complete EMI immunity, intrinsic electrical isolation (no ground loops or spark risks), operation in extreme high-voltage environments exceeding 100 kV, a 25+ year service life with zero maintenance and no recalibration requirements, and compact probe sizes (2–3 mm) suitable for confined installation spaces. Thermocouples and RTDs are susceptible to EMI, require complex multi-wire configurations, suffer from self-heating and drift over time, and cannot operate safely in high-voltage areas.
Q4: What types of equipment can be monitored with fiber optic temperature systems?
The systems are suitable for a wide range of applications including power transformers (dry-type and oil-immersed), switchgear and circuit breakers, GIS equipment, cable joints, generators, HVDC systems, power reactors, motor windings, VFDs, IGBT/SiC power devices, semiconductor processing equipment, industrial furnaces, MRI medical systems, battery energy storage, wind turbines, solar inverters, and aerospace equipment. Essentially, any application requiring accurate temperature monitoring in high-voltage, high-EMI, or harsh environments benefits from fiber optic sensing technology.
Q5: What is the measurement accuracy, temperature range, and response time?
The standard measurement accuracy is ±1°C, customizable for higher-precision applications. The temperature range spans –40°C to +260°C with customization available for extended ranges. Response time is under 1 second, enabling real-time detection of thermal events. Fiber optic cable lengths support 0 to 80 meters as standard, with custom extensions available. The system supports 1 to 64 monitoring channels per demodulator unit.
Q6: Is the installation of a fiber optic temperature monitoring system complex?
Installation is straightforward and can be completed by standard electrical technicians. The small probe diameter (2–3 mm) allows installation in confined spaces including transformer winding slots and switchgear contact points. INNO provides user-friendly monitoring software with tutorials and complete documentation. No routine maintenance, periodic calibration, or specialized tools are required during the system’s operational life, significantly reducing long-term labor and operating costs.
Q7: What are the cost benefits and expected return on investment?
The 25+ year service life with zero maintenance and calibration costs, combined with early hot-spot detection that prevents costly equipment failures and unplanned downtime, provides substantial economic value. Multi-channel monitoring capability (up to 64 channels per demodulator) reduces per-point costs for large installations. Most users report achieving full return on investment within 3–5 years through avoided failures, extended equipment life, and optimized maintenance scheduling.
Q8: Does INNO offer OEM/ODM and custom manufacturing services?
Yes, INNO provides comprehensive OEM private-label manufacturing and ODM co-development services. Customization options include branded product packaging, custom sensor probe configurations, tailored monitoring host specifications, fiber optic temperature measurement module development, RS485 interface customization, and cloud platform software development. The company also supports distributor programs and system integrator partnerships with dedicated technical and commercial support.
Q9: What certifications do INNO’s fiber optic temperature monitoring products hold?
All INNO products are manufactured under quality management systems certified to ISO 9001, ISO 14001, ISO 27001, and ISO 45001. Products hold CE and EMC certifications for international market compliance, along with RoHS certification for environmental standards. The company is committed to meeting evolving international compliance requirements and can discuss specific certification needs for particular markets or applications.
Q10: How can I get a quotation or technical consultation for my project?
Contact INNO directly via email at web@fjinno.net, WhatsApp or WeChat at +8613599070393, or phone at +8659183846499. The sales team provides one-on-one support with rapid quote response. You can also submit a product inquiry or request a customized quote through the company website at www.fjinno.net/contact. Provide details about your application type, number of monitoring points, installation environment, and any special requirements to receive an accurate, tailored quotation.
Fiber optic temperature sensor, Intelligent monitoring system, Distributed fiber optic manufacturer in China
 |
 |
 |